Drum Lifter Manufacturer Guide Types and Safety Tips

Are you struggling to find a reliable drum lifter manufacturer that can keep your facility safe while dramatically speeding up your operations? Transporting, rotating, and dumping heavy steel, plastic, or fiber drums is one of the most hazardous tasks in modern material handling—and using the wrong equipment will cost you time, money, and workplace safety.
In this ultimate guide, you’ll learn how to choose high-performance drum lifters, evaluate crucial features like load capacity and ATEX certification, compare hydraulic, electric, and manual drum positioners, and partner with a certified drum lifter manufacturer equipped with elite OEM/ODM engineering capabilities.
Let’s dive right in.
What is a Drum Lifter?
Definition and Operating Principles
A drum lifter is specialized material handling equipment designed to raise, transport, rotate, and position industrial drums safely. As a trusted drum lifter manufacturer, we build engineered lifting systems that secure 55-gallon steel, plastic, and fiber drums using mechanical jaws, hydraulic pressure, or attachments like a fork mounted drum lifter.
| Operating Principle | Mechanism | Primary Advantage |
|---|---|---|
| Rim Gripping Jaws | Automatic mechanical pressure applies grip force proportional to drum weight. | Slip-free lock on chime edges without manual clamping. |
| Hydraulic Assistance | Foot pedal or electric motor drives hydraulic fluid to raise high-capacity loads. | Smooth, effort-free vertical lifting with precise height control. |
| Fork Attachment | Slide-on sleeves lock directly onto standard forklift tines. | Instantly turns forklifts into heavy-duty drum handling units. |
Primary Functions in Material Handling
Modern drum handling solutions streamline operational workflows across busy industrial environments:
- Effortless Transport: Swiftly transfers heavy drums across warehouse floors and production bays.
- Precision Pouring: Rotates containers up to 360 degrees for controlled fluid dispensing and dumping.
- Vertical Stacking: Safely stacks drums onto high racks or pallets to maximize facility floor space.
- Multi-Container Versatility: Securely holds diverse rim profiles, including tight-head steel and open-head plastic containers.
Workplace Safety and Ergonomic Benefits
Integrating industrial drum lifters into daily operations directly eliminates severe manual handling hazards:
- Reduces Strain & Injury: Eliminates dangerous manual lifting, pushing, and rolling, protecting workers from severe spinal strain and musculoskeletal disorders.
- Prevents Spills & Drops: Heavy-duty positive locking clamps secure the load during transit, preventing costly material spills and hazardous leaks.
- Single-Operator Efficiency: Enables one operator to safely maneuver fully loaded containers, drastically boosting efficiency while lowering labor demands.
Key Features and Technical Specifications
As a direct drum lifter manufacturer, we build equipment engineered to meet rigorous industrial demands for safety, efficiency, and continuous operation. Every model balances precise control with rugged construction to optimize daily factory throughput.
Load Capacity and Lifting Height Options
We offer both custom and standard configurations designed to handle standard 55-gallon steel, plastic, and fiber drums. Our lifters integrate seamlessly alongside specialized drum handling equipment to streamline safe lifting, tilting, and transport tasks.
| Model Grade | Rated Capacity | Max Lifting Height | Primary Application |
|---|---|---|---|
| Light Duty | 300 kg (660 lbs) | Up to 1.5 m (5 ft) | Warehouse staging & short transfers |
| Standard Industrial | 500 kg (1,100 lbs) | Up to 2.5 m (8 ft) | Chemical processing & production lines |
| Heavy-Duty Power | 1,000 kg (2,200 lbs) | Up to 3.0 m (10 ft) | High-bay racking & heavy dispensing |
Safety Mechanisms and ATEX Certification
Operator protection guides our design choices. We build multiple fail-safe mechanisms directly into our lifting frames to minimize workplace hazards and chemical spills:
- Automatic Mechanical Grips: Dual-jaw clamping mechanisms lock securely onto the drum rim during elevation and auto-release upon touchdown.
- Overload Prevention: Integrated hydraulic relief valves prevent lifting beyond rated capacities.
- ATEX Certification: Non-sparking copper/brass contact surfaces and explosion-proof drive systems built for hazardous Zone 1 and Zone 2 environments.
- Floor Lock Brakes: Heavy-duty foot brakes lock the unit firmly during static load transfers.
Heavy-Duty Materials and Durable Construction
We construct core chassis structures using high-grade, heavy-gauge steel finished with acid-resistant powder coatings. For sanitary, cleanroom, or food-grade applications, we supply full 304 and 316 stainless steel builds. For facilities leveraging existing lift trucks, we also manufacture durable forklift attachments that expand material handling versatility, including dedicated fork mounted drum lifter options designed for heavy daily wear. drum lifter manufacturer
Common Types of Drum Lifting Equipment
Selecting the right drum handling machinery depends on your daily operational volume, ceiling clearance, and workflow demands. We engineer a full range of equipment tailored to handle different container styles and load capacities safely.
Manual, Hydraulic, and Electric Drum Lifters
- Manual Drum Lifters: Simple mechanical levers ideal for low-frequency operations, tight spaces, and budget-conscious setups.
- Hydraulic Drum Lifters: Utilize foot-pumps or hand-levers to lift standard steel, fiber, and plastic drums with minimal operator fatigue.
- Electric Drum Lifters: Feature fully powered drive and lift controls for high-throughput material handling environments, maximizing speed and plant productivity.
Drum Grippers, Grabbers, and Tong Lifters
- Rim-Grip Attachments: Automatically lock onto the top chime of the drum during lifting, maintaining a positive lock throughout transit.
- Tong Lifters: Heavy-duty, scissor-action clamps designed specifically for vertical overhead lifting of closed-head drums.
- Fork Mounted Drum Lifter Units: Slide directly onto standard forklift tines, turning standard lift trucks into efficient drum handling tools without needing extra machinery.
Drum Positioners, Rotators, and Dumpers
- Precision Dispensing: Features 180° to 360° manual or powered gear rotation for controlled pouring of viscous liquids and bulk powders.
- Multi-Angle Storage: Easily transitions drums between horizontal storage racks and vertical palletizing layouts.
- Integrated Batching: Compatible with digital scale systems to weigh, lift, and pour raw materials in a single workflow step.
Overhead Drum Lifters and Hoist Attachments
Overhead drum attachments connect to shop cranes, monorails, or hoists to move heavy barrels across crowded facility floors. When aisle space is limited, pairing hoist attachments with mobile workshop cranes for industrial lifting provides an ultra-versatile floor solution. You can also integrate specialty attachments with an all-electric mobile floor crane to transport heavy drums safely without relying on fixed overhead rail systems.
Industrial Application Scenarios
Chemical and Pharmaceutical Processing
In chemical and pharmaceutical plants, precision and contamination control are non-negotiable. We build specialized drum lifters using high-grade stainless steel and spark-resistant hydraulic systems to transfer volatile compounds, raw powders, and liquid ingredients cleanly and safely. drum lifter manufacturer
- Cleanroom Compliance: Smooth surfaces prevent particle buildup and simplify washdowns.
- Controlled Dosing: Precise 360-degree rotation allows exact pouring into mixing vats.
Oil, Gas, and Energy Sectors
Refineries, offshore rigs, and power plants deal with heavy steel barrels filled with lubricants, fuel, and dense chemicals. As an experienced drum lifter manufacturer, we produce heavy-duty equipment rated for harsh environments and continuous daily duty cycles.
- ATEX & Explosion-Proof: Non-sparking drum grippers and pneumatic lift options.
- High Payload Limits: Easily moves 55-gallon steel drums up to 1,500 lbs.
- All-Weather Durability: Corrosion-resistant coatings withstand tough marine and industrial atmospheres.
Warehousing, Logistics, and Manufacturing
High-speed distribution centers require fast, repeatable drum handling to maintain productivity. Attaching a fork mounted drum lifter to your existing lift truck fleet instantly converts standard vehicles into dedicated drum movers, cutting load times and improving safety. Explore our complete range of material handling equipment tailored for modern supply chain operations.
- Aisle Optimization: Compact designs allow tight maneuvering in narrow storage racks.
- Risk Reduction: Clamping mechanisms securely hold barrels, preventing drop hazards and ergonomic strain.
- Multi-Material Support: Handles steel, plastic, and fiber drums without manual adjustment.
How to Select the Right Drum Lifter
Selecting the right material handling equipment depends directly on your daily operational workflow, facility layout, and the specific containers you move. drum lifter manufacturer
Assessing Drum Types, Sizes, and Weights
Every drum material behaves differently under clamping pressure. Matching your drum handling gear to your exact inventory prevents container deformation and hazardous spills.
- Drum Material: Heavy-duty steel drums tolerate mechanical rim-clamping jaws easily. Soft plastic or fiber drums require wider, padded clamps or belt-wrapping mechanisms to distribute pressure evenly without crushing the container walls.
- Capacity & Volume: Standard 55-gallon (200L) drums weigh up to 800 kg (1,760 lbs) when filled with dense liquids. Always choose equipment rated at least 20% above your heaviest load.
- Attachment Style: If you already operate forklifts, using a fork mounted drum lifter allows for high-capacity transport without purchasing a standalone motorized lifter.
Evaluating Operational Environment and Space Constraints
Your physical workspace dictates the equipment footprint, frame style, and safety ratings required for daily use.
- Aisle Width & Turning Radius: Narrow warehouses demand compact straddle-leg or counterweighted designs that maneuver tight corners and slide directly under low-clearance pallets.
- Hazardous Zones: Facilities handling volatile chemicals or combustible dust require spark-proof, ATEX-compliant builds or fully air-powered systems.
- Custom Space Requirements: For facility floor plans with non-standard doorways or tight mezzanines, submit your dimensions through our contact page so our engineering team can adapt the chassis specifications.
Determining Power Source and Duty Cycle Needs
Match your lifter’s power system to your shift volume and operator throughput requirements. drum lifter manufacturer
- Manual & Hydraulic: Best for low-frequency operations (1–10 lifts per shift). Highly reliable, budget-friendly, and simple to maintain.
- Battery Electric: Built for high-throughput manufacturing plants moving dozens of drums every hour, eliminating manual effort and boosting lift speed.
- Pneumatic (Air-Powered): Ideal for continuous duty cycles in washdown environments, cleanrooms, and explosion-proof processing bays.
How to Choose a Reliable Drum Lifter Manufacturer
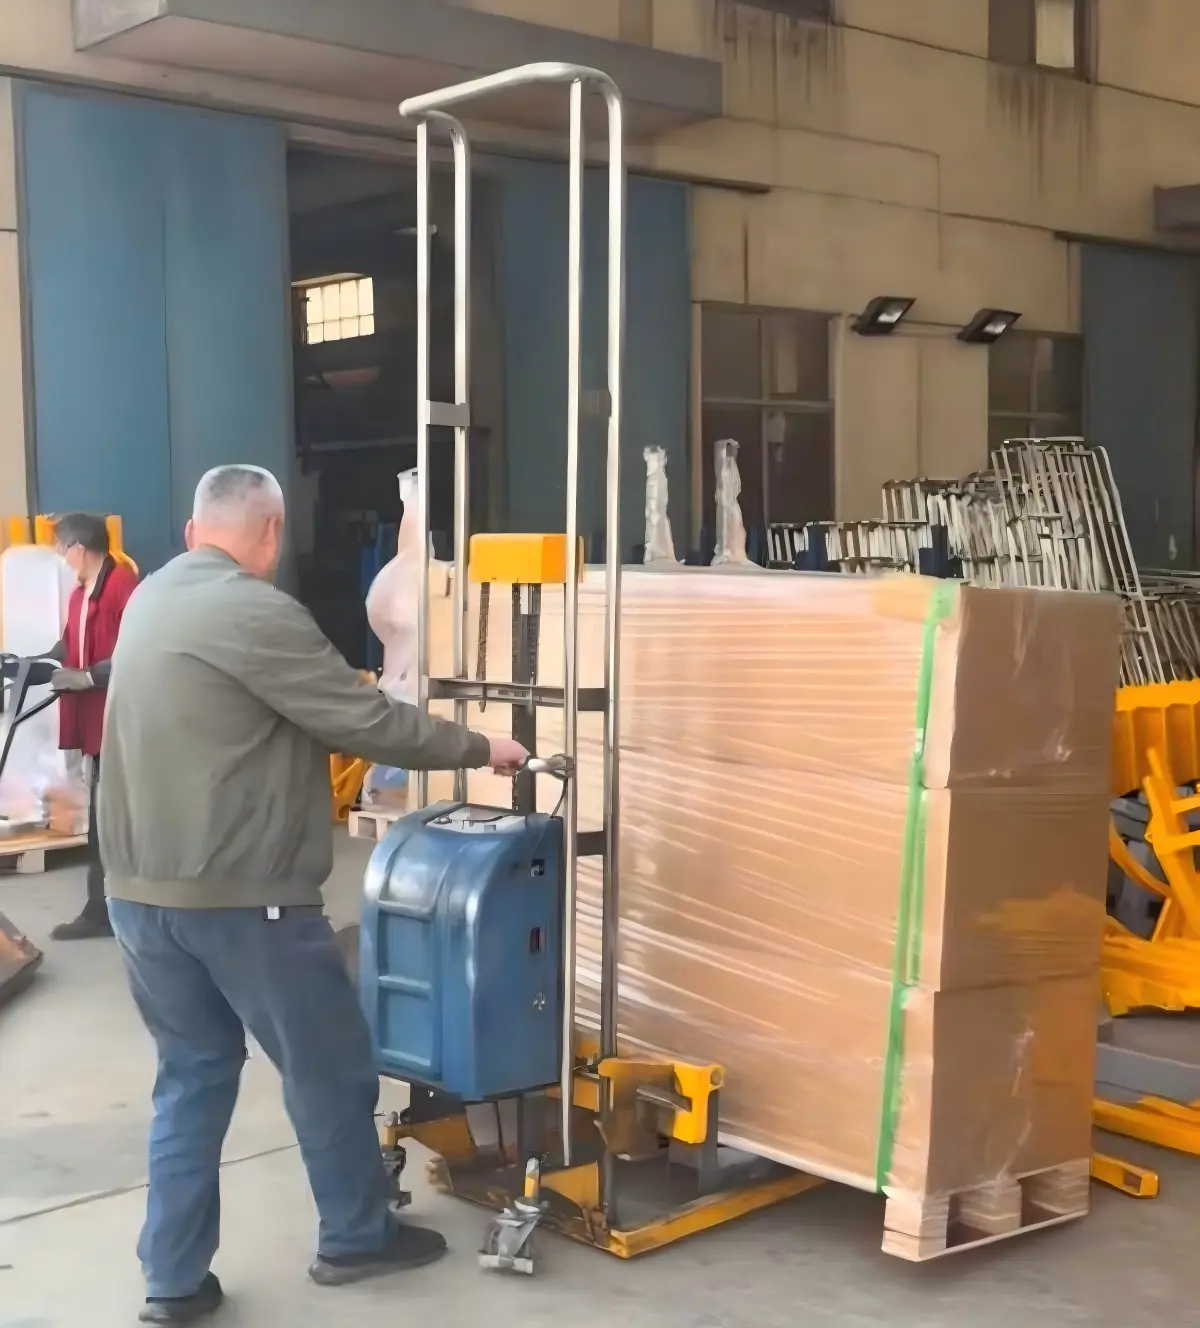
Selecting the right drum lifter manufacturer directly impacts facility safety, operational throughput, and long-term equipment maintenance costs. As an established industrial equipment supplier, we focus on delivering rugged units built to withstand demanding work environments.
Customization and OEM/ODM Engineering Capabilities
Standard models do not always fit unique plant layouts or specialized container specifications. We provide end-to-end OEM and ODM engineering services to tailor equipment to your exact operational requirements.
- Custom Clamping & Gripping Mechanisms: Adaptations for non-standard rim shapes, plastic drums, or delicate fiber containers.
- Custom Mount Options: Bespoke mounting plates for a specialized fork mounted drum lifter or hoist integration.
- Integrated Automation: Built-in weighing scales, precise pouring controls, and motorized rotational drives.
If you need tailored machinery built for your specific workflow, explore our full range of heavy-duty drum handling products.
Quality Certifications and Compliance Standards
High-risk lifting operations demand certified reliability. We maintain strict production protocols to guarantee every piece of equipment meets global safety standards.
| Certification / Standard | Core Focus & Application |
|---|---|
| ISO 9001:2015 | Ensures consistent quality management across all manufacturing stages. |
| CE Certification | Verifies full compliance with European health, safety, and safety directive standards. |
| ATEX Rating | Certified explosion-proof builds required for volatile chemical and oil operations. |
| OSHA Standards | Designed to satisfy strict ergonomic and mechanical load safety criteria. |
Wholesale Pricing, Warranty, and After-Sales Support
Working directly with an established manufacturer eliminates middleman markups while securing long-term technical backing for your facility fleet.
- Direct Wholesale Rates: Tiered pricing structures engineered for bulk fleet acquisitions and distributor partnerships.
- Multi-Year Warranty: Comprehensive structural and hydraulic system coverage backing every unit shipped.
- Fast-Track Spare Parts: Rapid global dispatch of seals, clamp pads, and hydraulic pumps to prevent facility downtime.
- Dedicated Technical Service: Direct access to engineering support for installation guidance and long-term maintenance of your material handling solutions.
Frequently Asked Questions About Drum Lifters
What is the maximum weight capacity of a standard drum lifter?
Standard drum lifting equipment typically handles load capacities between 500 lbs and 1,000 lbs (230 kg to 450 kg). Heavy-duty hydraulic models and specialized fork mounted drum lifters effortlessly handle heavier loads ranging from 1,500 lbs to 2,000 lbs (680 kg to 900 kg) per drum. As an established drum lifter manufacturer, we also build custom engineering solutions designed for custom high-capacity demands.
Can drum lifters handle plastic, steel, and fiber drums?
Yes, provided you choose the right gripping mechanism for your drum material:
- Steel Drums: Ideal for standard rim-clamping jaws, side clamps, and mechanical tong attachments.
- Plastic Drums: Require padded rim clamps or wide-surface pressure jaws to secure the flexible lip without damaging the container.
- Fiber Drums: Best secured using full-girth belly belts or specialized soft clamps to distribute pressure evenly and prevent structural crushing.
Always match your material handling equipment attachments to the specific container profile you handle daily.
How often should drum lifting equipment undergo maintenance inspection?
To maintain safe drum handling practices and protect your workforce, follow this inspection routine:
- Daily (Pre-Shift): Quick visual check of gripping jaws, welds, hydraulic lines, and safety latches.
- Monthly: Lubricate pivot points, check hydraulic fluid levels, and inspect stress points for hairline fractures or wear.
- Annually: Perform a thorough load test and complete safety audit in compliance with local industrial standards.